

What Are The Benefits Of Automatic Fermentation Towers?
Fermentation directly affects the volume, texture, and appearance of bread products. In large bakeries, managing this process manually becomes increasingly difficult as production quantities grow. Different fermentation durations, inconsistent environmental conditions, and repeated product handling can create variations between batches. These problems may affect downstream baking schedules and make it harder to maintain consistent finished products.
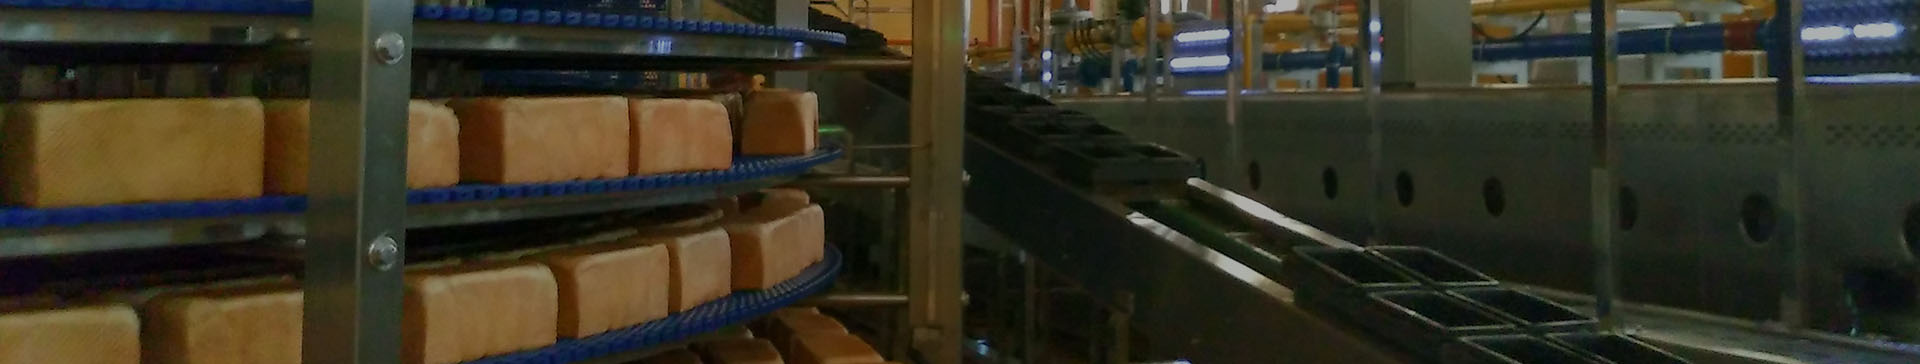
An Automatic Fermentation Tower addresses these challenges through controlled conveying and an adjustable fermentation environment. Dough pieces move through multiple levels while the system manages transportation time, temperature, and humidity. By connecting fermentation with upstream and downstream equipment, bakeries can establish a more organized and predictable production process.
How Does an Automatic Fermentation Tower Change Production?
Traditional batch fermentation often requires workers to load dough trays, arrange them inside a controlled room, and remove them after the required fermentation period.
An automatic tower uses a different operating method.
Dough pieces enter through an infeed conveyor and move through a continuous conveying path. The tower provides the required residence time while maintaining controlled environmental conditions. Once fermentation is completed, products are transferred to the next production stage.
This arrangement reduces repeated manual transfers and makes fermentation easier to coordinate with automatic dividing, shaping, and baking equipment.
Four Major Benefits for Industrial Bakeries
More Consistent Fermentation Conditions
Dough development depends on temperature, humidity, and fermentation time. Variations in these conditions may result in uneven expansion and different product volumes.
Automatic fermentation towers use environmental controls and conveyor speed adjustments to maintain more consistent operating conditions. For many conventional bread products, fermentation temperatures around 28–38°C and relative humidity around 75–85% can serve as initial reference ranges. Actual settings depend on dough formulation and product requirements.
Reduced Manual Handling
Automatic conveying reduces the need for workers to repeatedly move dough trays between processing areas.
This is particularly useful for continuous bakery lines where large quantities of dough pieces must be transferred at regular intervals. Less manual handling also helps reduce interruptions caused by loading and unloading activities.
Better Production Coordination
Fermentation time must match the operating speed of surrounding equipment. An automatic tower provides a controlled conveying path that can be adjusted according to production requirements.
For example, when the dividing machine increases its output, the fermentation system can be evaluated and adjusted to maintain sufficient holding capacity and residence time.
More Efficient Use of Factory Space
A vertical tower structure provides a long conveying route within a relatively compact floor footprint. This can be valuable in factories where ovens, cooling systems, and packaging machines already occupy considerable space.
What Determines the Performance of an Automatic Tower?
The benefits depend on correct equipment configuration. Several factors influence actual operating performance.
| Design Factor | Effect on Production |
|---|---|
| Conveyor speed | Determines fermentation residence time |
| Tower capacity | Controls the number of dough pieces accommodated |
| Temperature control | Influences yeast activity |
| Humidity control | Helps prevent surface drying |
| Air circulation | Supports environmental uniformity |
| Feeding arrangement | Maintains stable product spacing |
These factors must be evaluated together. Increasing conveyor capacity without checking airflow or environmental distribution may create inconsistent fermentation results.
How to Integrate the Tower Into an Existing Bakery Line
Successful integration starts with matching the tower to the upstream dough preparation equipment and downstream processing requirements.
The infeed section should receive dough pieces at a stable rate. Conveyor transfers should avoid unnecessary product movement, while the discharge section must connect smoothly with the next machine.
Manufacturers should also confirm installation height, cleaning access, electrical requirements, and maintenance arrangements before finalizing the layout.
KC-SMART considers these production conditions when planning automatic fermentation equipment for industrial bakery applications.
Is Automatic Fermentation Suitable for Every Bakery?
Automatic towers are particularly useful for bakeries with standardized products, continuous production schedules, and relatively stable output requirements.
Smaller facilities producing many different products in limited batches may prefer a fermentation room because it offers greater scheduling flexibility.
The decision should be based on production volume, product variety, available space, labor requirements, and the degree of automation needed.
Conclusion
Automatic fermentation towers help industrial bakeries improve environmental consistency, reduce manual handling, coordinate production processes, and utilize factory space more efficiently. Their effectiveness depends on matching conveyor capacity, temperature, humidity, and fermentation time with actual dough characteristics. A properly configured Automatic Fermentation Tower supports a more stable and organized bakery production workflow.